Direct manufacturer supply for international fashion luxury houses, high-end footwear brands, and premium retail distribution networks. Fully certified and customized to exact technical specifications.
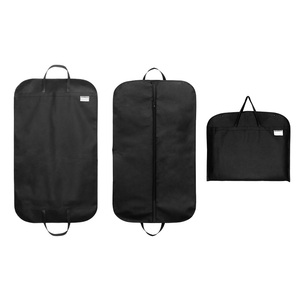
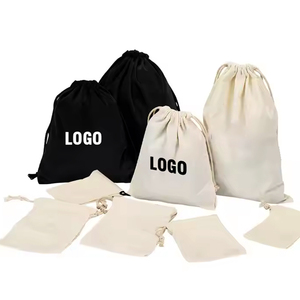
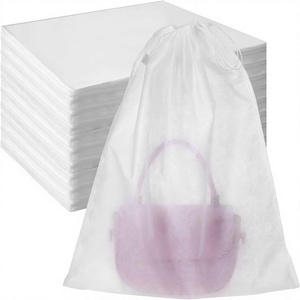
As global supply chains adjust to carbon border taxes, zero-landfill mandates, and heightened luxury consumer expectations, procurement directors must adapt their OEM/ODM strategies.
Global retail conglomerates are moving away from unverified blended fibers. Procurement workflows now demand certified supply chains: GOTS-certified organic cotton, OEKO-TEX Standard 100 chemical neutrality, and post-consumer recycled poly (GRS). Dust bags are no longer treated as disposable shipping liners; they are integrated secondary packaging evaluated under rigorous corporate social responsibility matrices.
Modern luxury leather items, including aniline-dyed calves and vegetable-tanned hides, are susceptible to humidity degradation, color transfer, and finish stripping. Leading brands now require custom dust bags with optimized breathability parameters. High-density twill weaves and microfiber linings protect delicate metallic hardware from oxidation without sealing in moisture, preventing fungal spore incubation during maritime transit.
With high-speed automated sorting in multi-brand 3PL fulfillment hubs, variation in dust bag dimensions leads to pallet packing failures and damaged boxed goods. Industrial procurement protocols require automated precision fabric cutting with stitch tolerance controls under ±2mm, reinforced flat-lock seams, and pull-tested closure drawstrings rated for high tensile cycles.
Compare physical performance specifications, fabric behavior, and appropriate applications for your production runs.
| Material Categorization | Standard Areal Density | Tensile & Vapor Profile | Primary Luxury Segment | Recommended Brand Decor |
|---|---|---|---|---|
| Carded Virgin Cotton Muslin | 120 – 160 GSM | High air permeability, moderate abrasion protection, natural matte hand-feel. | Luxury Leather Purses, Designer Shoes, Fine Millinery | Water-based Screen Printing, Subtle Tone-on-Tone Heat Stamp |
| Combed Cotton Twill (High-Density) | 240 – 350 GSM | Exceptional structural integrity, low lint shedding, soft interior non-abrasive face. | High-End Handbags, Structured Briefcases, Luxury Luggage | Precision High-Density Screen Print, Jacquard Woven Trim, Monogram Embroidery |
| Spunbond Polypropylene (Non-Woven) | 70 – 120 GSM | Hydrophobic barrier, cost-efficient bulk production, ultra-lightweight. | Suit Covers, Mass-Market Footwear, Department Store Transit | Direct Flexographic Imprint, Single-Color Screen Print |
| Post-Consumer Recycled Poly (RPET) | 150 – 280 GSM | Tear-resistant, water-resistant, traceable GRS chain-of-custody documentation. | Contemporary Eco-Luxury, Athletic Gear, Cosmaceuticals | Dye Sublimation, Heat Transfer Film, Silicon Label Badging |
| Double-Faced Plush Flannel / Suede | 180 – 260 GSM | Maximum hardware protection, static-dissipative qualities, heavy luxury weight. | High Jewelry, Exotic Skin Handbags, Luxury Timepieces | Metallic Foil Stamping, Debossed Leather Applique, Silk Braided Pulls |
By bypassing sourcing middlemen and trading agents, you gain direct engineering access to our integrated manufacturing facilities.
From raw spun cotton sourcing to high-precision computerized cutting, our fully owned manufacturing workshops ensure control over every lot. Fabric shrinkage rates, colorfastness, and dimensional tolerances are audited systematically prior to final stitching.
Protect valuable white and pastel luxury leathers from dangerous phthalate plasticizers and colorant bleeding. We use strictly regulated, non-migrating, solvent-free screen-printing inks that easily pass REACH and California Proposition 65 testing standards.
Eliminate risk before initiating mass scale runs. Receive custom-patterned, branded, real-material counter-samples within 3 to 5 business days for physical fit checks, hardware scratch testing, and retail review approval.
Full-container (FCL) or grouped pallet (LCL) freight is managed through in-house documentation teams. We prepare dual-language packing declarations, certified bills of lading, and preferential certificates of origin to keep your customs clearance moving smoothly.
Precision-engineered quality assurance embedded across every manufacturing milestone.
Raw greige yarns are scoured, bleached, and woven to strict areal weights. Textiles undergo heat pre-shrinking and singeing treatments to eliminate excess lint, preventing unwanted fiber transfer onto velvet, suede, or polished box-calf items.
High-precision laser tables cut patterns with heat-sealed or fray-resistant edges. Graphics are placed using automated silk-screen machines with calibrated tension screens, followed by infrared heat tunnels to ensure proper ink curing and color fastness.
Skilled operators assemble dust bags with reinforced bar-tacks and durable drawstrings. Every finished bag passes through high-sensitivity needle detection equipment before carton pack-out, eliminating stray metal fragments.
Everything your sourcing and supply chain team needs to know regarding factory-direct wholesale runs.
Send your tech packs, target sizing, and volume forecasts directly to our factory floor. Our packaging engineers reply with material recommendations and custom quotations within 24 hours.
Send an Inquiry